Why Resin Molds Often Short-Pour:
Specific Gravity & Density Explained
Published on March 28, 2026 • By MakerRatio Studio Team • Calibrated to Official TDS Density Data
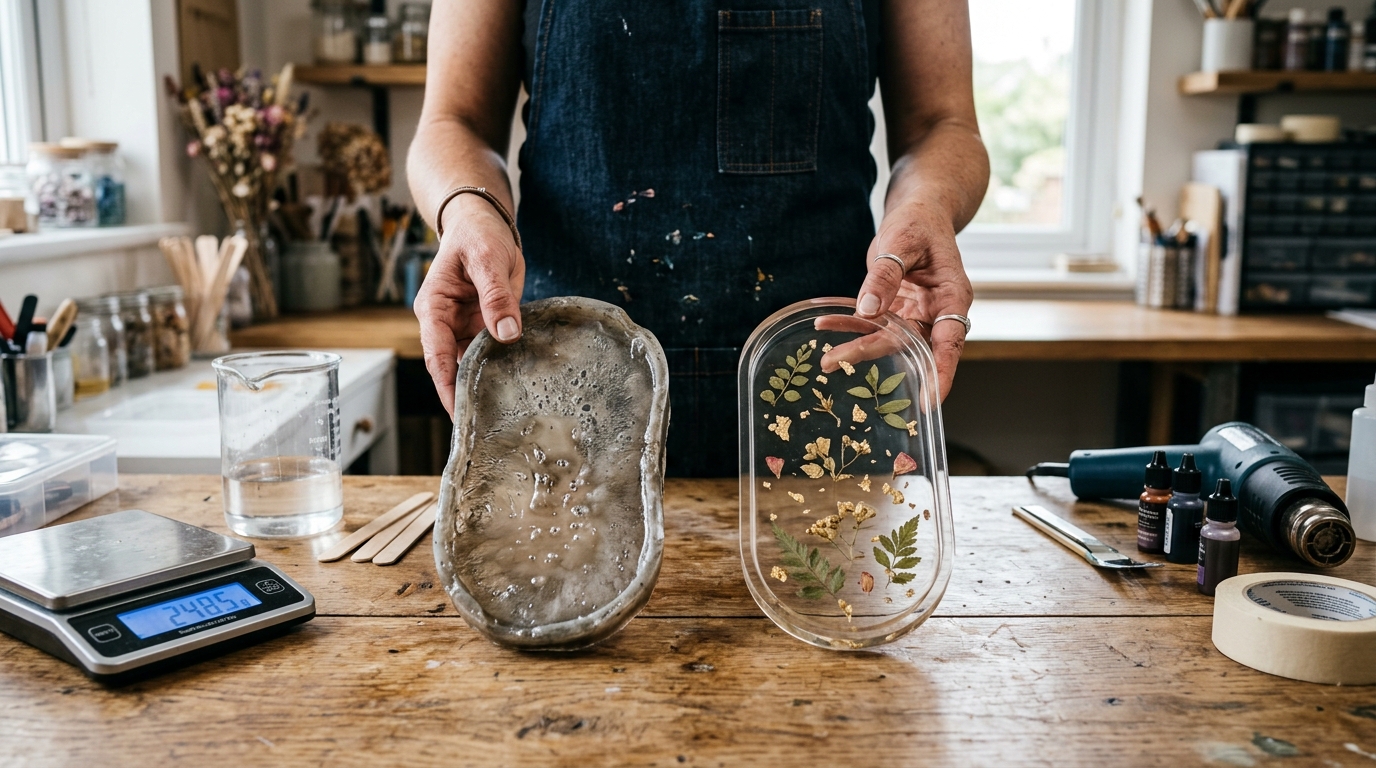
Visual Demonstration: A short-poured sunken casting caused by water volume error (left) vs a mathematically calibrated density pour (right).
Calculate Your Exact Resin Grams Instantly
Stop guessing volume lines. Input your mold dimensions and select your resin brand density to get exact Part A and Part B weights in 3 seconds.
Few craft mistakes are as common or expensive as short-pouring silicone molds.
You carefully measure your silicone mold cavity, calculate 500ml of volume, weigh out 500 grams of liquid on a digital scale... and yet, when the casting cures, the top edge is noticeably sunken with a concave lip that ruins the finished piece.
If you have poured resin, Jesmonite, or craft concrete, you know this exact frustration. Where does the missing volume go? Did the resin evaporate? Did the silicone expand?
Industrial polymer chemistry confirms the underlying reason: "Water math is lying to you."
The Hidden "Density Deficit" (Why 1ml Does NOT Equal 1g)
When crafters estimate resin volume, almost everyone relies on the standard universal rule: 1 milliliter = 1 gram, or attempts to fill molds with tap water without multiplying by specific gravity. If you use water to find mold capacity, you must use the calibrated digital scale tare method (see our step-by-step Water Displacement Mold Volume Guide). Similarly, if you cast from 3D printed models, slicer volumes must be scaled by density (see our complete guide on Converting STL Volume to Resin & Silicone Weight).
Water has a specific gravity (density) of exactly 1.00 g/ml at room temperature.
However, liquid epoxy resins, hardeners, silicone rubber, and Jesmonite composites are significantly heavier and denser than water:
| Material Type | Specific Gravity (Density) | 500ml Mold = Real Weight Needed | Hidden Deficit |
|---|---|---|---|
| Pure Tap Water | 1.00 g/ml | 500.0 grams | 0g (Baseline) |
| Tabletop Epoxy Resin | 1.12 g/ml | 560.0 grams | -60.0g (Short Pour!) |
| Deep Pour River Table Epoxy | 1.08 g/ml | 540.0 grams | -40.0g |
| Jesmonite AC100 Composite | 1.75 g/ml | 875.0 grams | -375.0g |
| Craft Mortar / Concrete | 2.10 g/ml | 1,050.0 grams | -550.0g |
Look at that table again.
If you pour a 500ml mold using standard epoxy resin (1.12 g/ml) and mix 500 grams by weight on your scale, you are short by 60 full grams of material. That 60-gram deficit is the exact reason your edges collapse and your surfaces curve inward as the epoxy cures.
The 3-Second Density Formula
To get a crystal-clear, perfectly flat casting every single time, you must correct for your material's specific density and add a 5% safety buffer for container wall cling.
Real-World Calculation Example:
- Mold Volume: 250 ml (Circular Coaster Mold)
- Resin Brand Density: 1.10 g/ml (ArtResin Preset)
- Math: 250 × 1.10 = 275g × 1.05 (wall buffer) = 288.7 grams total mixed weight.
Calculate Your Mold Shapes Free
3 Core Rules to End Short Pours Forever
1. Never Trust Printed Graduation Marks on Plastic Cups
Printed volume lines on cheap plastic mixing cups can be off by up to 10%. A 5ml error in Part B hardener can leave your casting rubbery or tacky forever. Always weigh your Part A and Part B on a 0.01g digital scale.
2. Overfill by 1mm (The Meniscus Rule)
Liquid surface tension pulls epoxy slightly up silicone walls. Overfill by 1mm past the rim to compensate for thermal shrinkage as the exothermic reaction cools.
3. Use Brand-Specific Density Profiles
Deep-pour resins are thinner (lower density ~1.08 g/ml), while quick-cure dome resins are thick (higher density ~1.14 g/ml). Always check density specs before pouring large batches.
Related Mold Making & Volume Guides
Stop guessing your resin weights. Calculate your exact recipe before you crack open your next bottle of hardener!